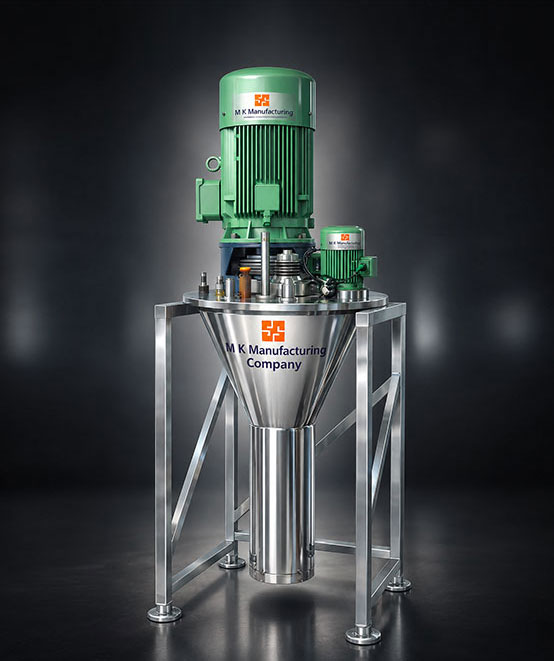
Rustom Rotary Disk Atomizers are specially engineered to convert liquid feed into fine, uniform droplets during the spray-drying process.
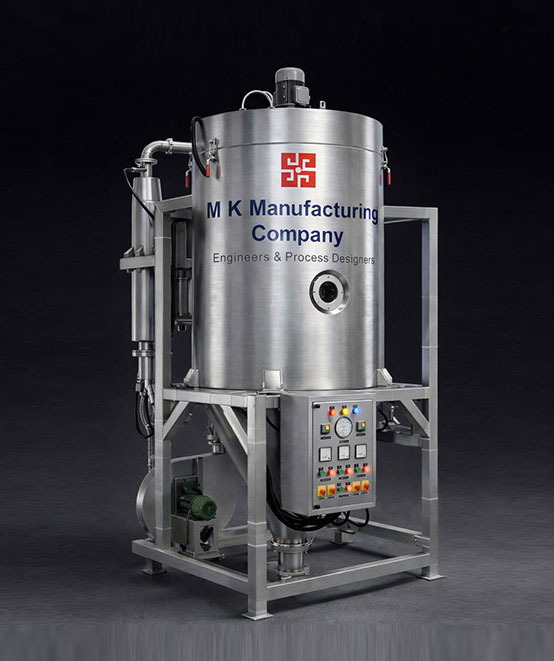
Our Pilot Spray Dryer is a compact and portable system designed for laboratory research, pilot trials and small-scale production.
Our Milk Processing Plants are designed to handle every stage of dairy production, from milk reception and filtration to pasteurization.
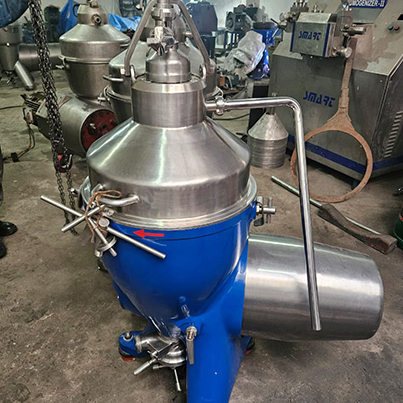
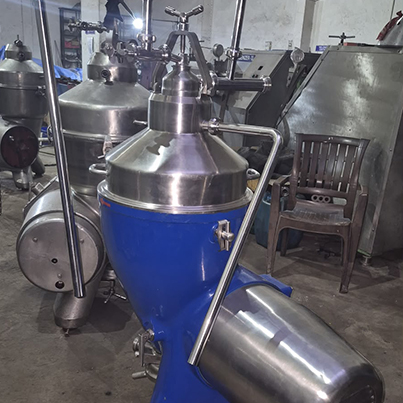
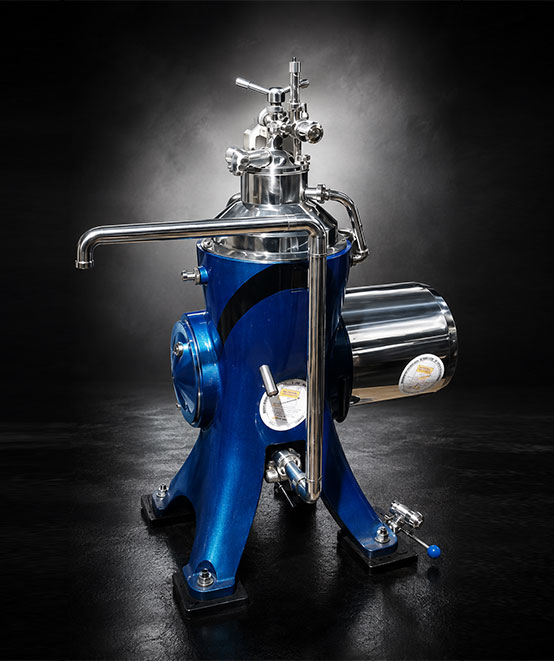
Our cream separators are engineered to hygienically and efficiently separate cream from milk using high-speed centrifugal force.
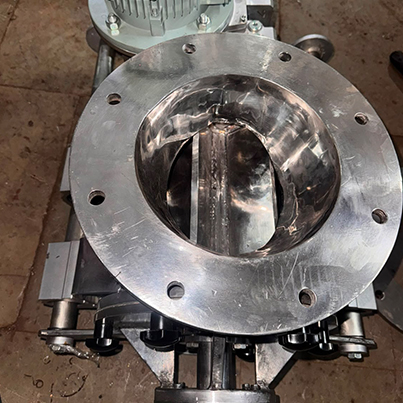
Our Rotary Airlock Valve is engineered to provide smooth and consistent material discharge while minimizing air leakage in pneumatic conveying systems.
We have developed an Atomizer which Agglomerates the product (Powder) For example: Recycling the fine from cyclone and again spraying through Atomizer with feed. As for concentrated feed there is Liquid distributor. As for same there is another distributor for fine powder which will distribute the fine powder is correct proposition and liquid will nowhere come in contact with fine powder before atomizing. The thing is when the atomizer wheel (Disk) spray the concentrated feed at same time and same RPM it will spray fine powder. In this stage we can agglomerate the powder very nicely. We can also agglomerate powder for chemical & pharmaceutical product. As now we have taken trial on whey Milk Powder & skim Milk Powder which is 100% success. As we have designed this Atomizer and completely successfully we have taken trial in India. Also Atomizer specially designed with continuously oil lubrication system for bearing as there is filter for oil, buzzer and oil lamp indicator for atomizer safety. Atomizer have a capacity of 5 liter oil storage for which we can change every after 7 month only after continuous running of machine.
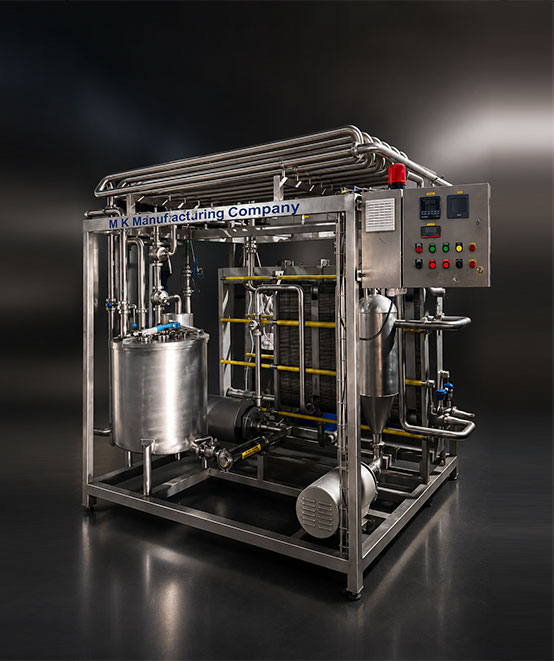
MK Manufacturing Company provides complete turnkey solutions for milk processing plants, from milk reception and chilling to pasteurization, homogenization, storage and final packing. Our dairy processing systems are designed using food-grade stainless steel construction, hygienic piping, efficient heat-transfer systems and automation options to provide reliable, hygienic and economical milk processing. We design and manufacture plants according to the customer's required capacity, product range, available space, utilities and level of automation.
We offer cream separators in multiple capacities to accommodate different production requirements:
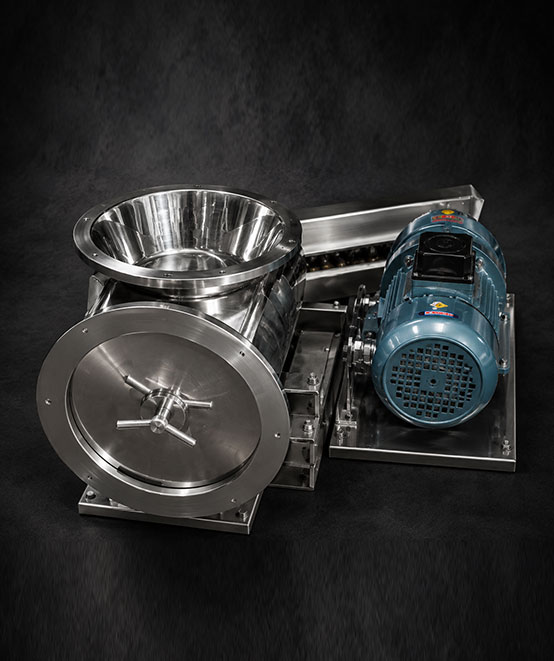
Our Rotary Air Lock Valves are designed for controlled discharge and continuous feeding of powders, granules, and bulk materials from hoppers, silos, cyclones, filters, and conveying systems. They help maintain a controlled material flow while minimizing air leakage between different pressure zones.
Rotary Air Lock Valves are available in different sizes and capacities to suit various material-handling requirements:
Our Cream Separators are engineered to separate cream from milk efficiently, helping dairy processors achieve consistent results while maintaining a smooth and dependable production process. Designed for different scales of operation, these machines can be selected according to the required milk-handling capacity and processing setup. From smaller dairy operations to high-volume processing facilities, our range of cream separators provides a practical solution for controlled and efficient cream recovery.
We offer cream separators in multiple capacities to accommodate different production requirements:
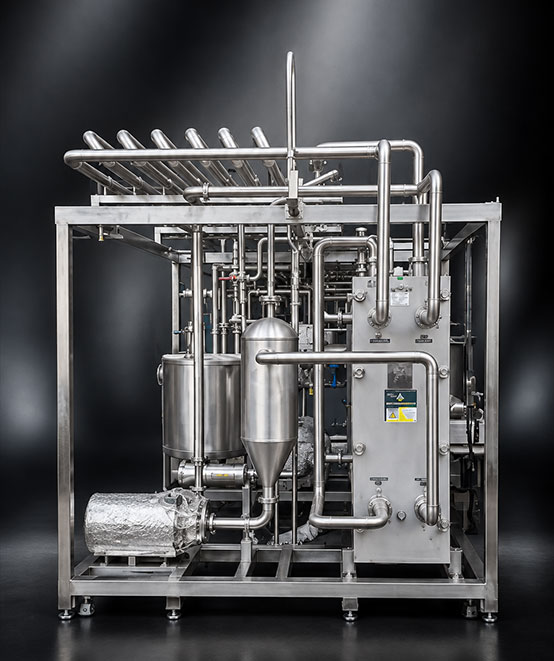
Our Milk Pasteurizers are designed to provide controlled heat treatment of milk, helping dairy processors improve product safety, consistency, and shelf life while preserving the desired quality of the milk.
Available in different capacities, our pasteurization systems can be configured for small dairy operations as well as commercial and industrial milk processing facilities. Each system can be selected according to production volume, process requirements, and plant layout.
We offer Milk Pasteurizers in different processing capacities to suit varying dairy production requirements:
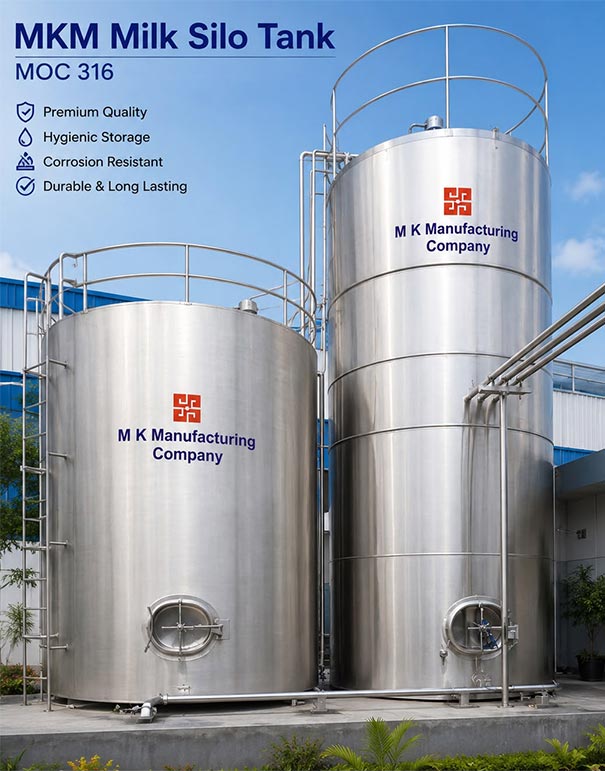
Our SS Silo Tanks are designed for safe and hygienic storage of milk, dairy products, beverages, food ingredients, and other compatible liquids. Manufactured from quality stainless steel, these tanks offer durability, easy cleaning, and efficient use of floor space.
We offer SS Silo Tanks in different capacities to suit various production requirements: